May 13, 2026

Table of Contents 1.High-Pressure Reactor Safety: The Core of Laboratory Safe Reaction Equipment 2.Dual-Valve System: The First Line of Defense for High-Pressure Reactor Safety 3.Reactor Automatic Pressure Relief: Key Protection Against Overpressure 4.Real-Time Pressure Monitoring: Core Means of Safety Early Warning 5.Integrated Safety System Construction of Laboratory Safe Reaction Equipment 6.Performance Comparison of Key Safety Components 7.Industry-Related FAQs 1. High-Pressure Reactor Safety: The Core of Laboratory Safe Reaction Equipment High-pressure reactors are essential equipment in chemical, pharmaceutical, and material science laboratories. They operate under extreme pressure and temperature conditions, making high-pressure reactor safety a top priority for laboratory operations. According to the U.S. Chemical Safety and Hazard Investigation Board (CSB), uncontrolled pressure and temperature in reactors have led to catastrophic accidents. A 2007 explosion at a Florida chemical company, for example, killed four workers and injured a dozen more, with the reactor’s 3-inch-thick steel walls ruptured by pressure reaching several thousand pounds per square inch. Laboratory safe reaction equipment, especially high-pressure reactors, requires a comprehensive safety system to prevent such disasters. This system mainly consists of three core components: dual-valve system, reactor automatic pressure relief, and real-time pressure monitoring. Together, they form a multi-layered safety barrier. 2. Dual-Valve System: The First Line of Defense for High-Pressure Reactor Safety 2.1 Working Principle of Dual-Valve System The dual-valve system, also known as the safety dual valve, is an integrated control component with two independent and linked valve cores in the same valve body. It adopts a redundant design, which means both valves must act simultaneously to maintain normal operation. During normal operation, both solenoid valves are energized, and the pilot pressure pushes the dual main valve cores to switch synchronously, ensuring the reactor’s pressure is stable. If either valve fails—such as coil burnout or valve core jamming—the other valve cannot establish effective pressure alone, and the system immediately enters a safe shutdown state. 2.2 Safety Advantages and Performance Data of Dual-Valve System The biggest advantage of the dual-valve system is its high safety redundancy, which eliminates accidents caused by single-point failures. Its failure exhaust time is as short as 0.05 to 0.07 seconds, much faster than traditional single-valve systems. Statistics show that laboratories using dual-valve systems have a 92% lower risk of pressure leakage accidents compared to those using single-valve systems. This data is verified by industrial safety tests conducted by multiple authoritative institutions. 3. Reactor Automatic Pressure Relief: Key Protection Against Overpressure 3.1 Trigger Mechanism of Automatic Pressure Relief System The reactor automatic pressure relief system is a critical active protection device designed to prevent overpressure. Its core function is to automatically and quickly release pressure without manual intervention when the internal pressure exceeds the preset safety threshold. The system usually sets multiple pressure thresholds, including early warning threshold, action threshold, and emergency cutoff threshold. The action threshold is generally set to 105% to 110% of the reactor’s maximum allowable working pressure (MAWP), leaving sufficient safety margin. When the pressure exceeds the action threshold, the system immediately activates the actuator—usually a pilot-operated safety valve or electromagnetic pressure relief valve—to release pressure rapidly, preventing the reactor from rupturing. 3.2 Performance of Automatic Pressure Relief System The response time of a high-quality automatic pressure relief system is typically within 100 milliseconds, and some advanced models can even reach 2 milliseconds, ensuring that pressure is released in time before dangerous levels are reached. Unlike traditional manual pressure relief methods, the automatic system avoids human error caused by delayed operation. In fact, 80% of overpressure accidents in laboratories are related to delayed manual pressure relief, according to a survey by the European Laboratory Safety Association (ELSA). 4. Real-Time Pressure Monitoring: Core Means of Safety Early Warning 4.1 Technical Principle of Real-Time Pressure Monitoring Real-time pressure monitoring is the "eye" of the high-pressure reactor safety system. It uses high-precision pressure sensors—such as piezoelectric or strain gauge sensors—to collect dynamic pressure signals inside the reactor in real time. The collected signals are filtered and amplified by a signal conditioning circuit, then sent to a safety controller for millisecond-level comparison with preset thresholds. If the pressure changes abnormally, the system will issue an alarm immediately and trigger the automatic pressure relief system if necessary. 4.2 Monitoring Accuracy and Response Performance The monitoring accuracy of professional real-time pressure monitoring systems can reach ±0.1 psi, which is sufficient to detect subtle pressure changes that may lead to dangerous situations. The data transmission delay is less than 50 milliseconds, ensuring that operators can grasp the reactor’s pressure status in real time. For laboratories dealing with flammable and explosive materials, real-time pressure monitoring is particularly important. It can predict pressure surges in advance, providing valuable time for operators to take emergency measures. 5. Integrated Safety System Construction of Laboratory Safe Reaction Equipment 5.1 Coordinated Work Logic of Multi-Systems The safety of high-pressure reactors cannot rely on a single component. The dual-valve system, automatic pressure relief, and real-time pressure monitoring work together to form a complete safety guarantee system. The real-time pressure monitoring system acts as the first warning line, detecting abnormal pressure changes. The dual-valve system maintains stable pressure during normal operation and cuts off the system in case of failure. The automatic pressure relief system is the last line of defense, preventing overpressure accidents when other systems fail. 5.2 Safety Standards and Application Cases Laboratory safe reaction equipment, including high-pressure reactors, must comply with relevant international standards. For example, China’s national standard GB/T 32708-2016 specifies strict safety requirements for laboratory reactors, covering pressure resistance, temperature limits, and interlock protection. A pharmaceutical laboratory in Germany upgraded its high-pressure reactor safety system with the three core components mentioned above. After one year of operation, the number of safety hidden dangers decreased by 95%, and no pressure-related accidents occurred. 6. Performance Comparison of Key Safety Components Safety Component Response Time Failure Rate Safety Improvement Rate Dual-Valve System 0.05-0.07s 0.3% 92% Automatic Pressure Relief System 2ms-100ms 0.5% 88% Real-Time Pressure Monitoring ≤50ms 0.2% 90% Traditional Single-Valve System 0.5-1s 8.7% 45% 7. Industry-Related FAQs Q1: What is the core difference between a dual-valve system and a single-valve system? A1: The dual-valve system adopts a redundant design with two independent valve cores. Both valves must act simultaneously to work normally, and any valve failure will trigger a safe shutdown. The single-valve system has only one valve core, which is prone to single-point failures, leading to pressure leakage or overpressure. Q2: What is the reasonable setting range for the action threshold of the automatic pressure relief system? A2: The action threshold is generally set to 105% to 110% of the reactor’s maximum allowable working pressure (MAWP). This setting can avoid false triggering caused by slight pressure fluctuations and ensure that pressure is released in time before reaching dangerous levels. Q3: How often should the real-time pressure monitoring system be calibrated? A3: It is recommended to calibrate the system every 6 months. For laboratories dealing with highly dangerous materials, calibration should be carried out every 3 months to ensure monitoring accuracy. Calibration should be performed by professional institutions in accordance with relevant standards. Q4: Can the three core safety components work independently? A4: They can work independently, but the safety effect will be greatly reduced. The real-time pressure monitoring system can only issue alarms, the dual-valve system can only maintain normal pressure and cut off failures, and the automatic pressure relief system can only release overpressure. Only when they work together can a comprehensive safety barrier be formed.
Table of Contents 1.High-Pressure Reactor Safety: The Core of Laboratory Safe Reaction Equipment 2.Dual-Valve System: The First Line of Defense for High-Pressure Reactor Safety 3.Reactor Automatic Pressure Relief: Key Protection Against Overpressure 4.Real-Time Pressure Monitoring: Core Means of Safety Early Warning 5.Integrated Safety System Construction of Laboratory Safe Reaction Equipment 6.Performance Comparison of Key Safety Components 7.Industry-Related FAQs 1. High-Pressure Reactor Safety: The Core of Laboratory Safe Reaction Equipment High-pressure reactors are essential equipment in chemical, pharmaceutical, and material science laboratories. They operate under extreme pressure and temperature conditions, making high-pressure reactor safety a top priority for laboratory operations. According to the U.S. Chemical Safety and Hazard Investigation Board (CSB), uncontrolled pressure and temperature in reactors have led to catastrophic accidents. A 2007 explosion at a Florida chemical company, for example, killed four workers and injured a dozen more, with the reactor’s 3-inch-thick steel walls ruptured by pressure reaching several thousand pounds per square inch. Laboratory safe reaction equipment, especially high-pressure reactors, requires a comprehensive safety system to prevent such disasters. This system mainly consists of three core components: dual-valve system, reactor automatic pressure relief, and real-time pressure monitoring. Together, they form a multi-layered safety barrier. 2. Dual-Valve System: The First Line of Defense for High-Pressure Reactor Safety 2.1 Working Principle of Dual-Valve System The dual-valve system, also known as the safety dual valve, is an integrated control component with two independent and linked valve cores in the same valve body. It adopts a redundant design, which means both valves must act simultaneously to maintain normal operation. During normal operation, both solenoid valves are energized, and the pilot pressure pushes the dual main valve cores to switch synchronously, ensuring the reactor’s pressure is stable. If either valve fails—such as coil burnout or valve core jamming—the other valve cannot establish effective pressure alone, and the system immediately enters a safe shutdown state. 2.2 Safety Advantages and Performance Data of Dual-Valve System The biggest advantage of the dual-valve system is its high safety redundancy, which eliminates accidents caused by single-point failures. Its failure exhaust time is as short as 0.05 to 0.07 seconds, much faster than traditional single-valve systems. Statistics show that laboratories using dual-valve systems have a 92% lower risk of pressure leakage accidents compared to those using single-valve systems. This data is verified by industrial safety tests conducted by multiple authoritative institutions. 3. Reactor Automatic Pressure Relief: Key Protection Against Overpressure 3.1 Trigger Mechanism of Automatic Pressure Relief System The reactor automatic pressure relief system is a critical active protection device designed to prevent overpressure. Its core function is to automatically and quickly release pressure without manual intervention when the internal pressure exceeds the preset safety threshold. The system usually sets multiple pressure thresholds, including early warning threshold, action threshold, and emergency cutoff threshold. The action threshold is generally set to 105% to 110% of the reactor’s maximum allowable working pressure (MAWP), leaving sufficient safety margin. When the pressure exceeds the action threshold, the system immediately activates the actuator—usually a pilot-operated safety valve or electromagnetic pressure relief valve—to release pressure rapidly, preventing the reactor from rupturing. 3.2 Performance of Automatic Pressure Relief System The response time of a high-quality automatic pressure relief system is typically within 100 milliseconds, and some advanced models can even reach 2 milliseconds, ensuring that pressure is released in time before dangerous levels are reached. Unlike traditional manual pressure relief methods, the automatic system avoids human error caused by delayed operation. In fact, 80% of overpressure accidents in laboratories are related to delayed manual pressure relief, according to a survey by the European Laboratory Safety Association (ELSA). 4. Real-Time Pressure Monitoring: Core Means of Safety Early Warning 4.1 Technical Principle of Real-Time Pressure Monitoring Real-time pressure monitoring is the "eye" of the high-pressure reactor safety system. It uses high-precision pressure sensors—such as piezoelectric or strain gauge sensors—to collect dynamic pressure signals inside the reactor in real time. The collected signals are filtered and amplified by a signal conditioning circuit, then sent to a safety controller for millisecond-level comparison with preset thresholds. If the pressure changes abnormally, the system will issue an alarm immediately and trigger the automatic pressure relief system if necessary. 4.2 Monitoring Accuracy and Response Performance The monitoring accuracy of professional real-time pressure monitoring systems can reach ±0.1 psi, which is sufficient to detect subtle pressure changes that may lead to dangerous situations. The data transmission delay is less than 50 milliseconds, ensuring that operators can grasp the reactor’s pressure status in real time. For laboratories dealing with flammable and explosive materials, real-time pressure monitoring is particularly important. It can predict pressure surges in advance, providing valuable time for operators to take emergency measures. 5. Integrated Safety System Construction of Laboratory Safe Reaction Equipment 5.1 Coordinated Work Logic of Multi-Systems The safety of high-pressure reactors cannot rely on a single component. The dual-valve system, automatic pressure relief, and real-time pressure monitoring work together to form a complete safety guarantee system. The real-time pressure monitoring system acts as the first warning line, detecting abnormal pressure changes. The dual-valve system maintains stable pressure during normal operation and cuts off the system in case of failure. The automatic pressure relief system is the last line of defense, preventing overpressure accidents when other systems fail. 5.2 Safety Standards and Application Cases Laboratory safe reaction equipment, including high-pressure reactors, must comply with relevant international standards. For example, China’s national standard GB/T 32708-2016 specifies strict safety requirements for laboratory reactors, covering pressure resistance, temperature limits, and interlock protection. A pharmaceutical laboratory in Germany upgraded its high-pressure reactor safety system with the three core components mentioned above. After one year of operation, the number of safety hidden dangers decreased by 95%, and no pressure-related accidents occurred. 6. Performance Comparison of Key Safety Components Safety Component	Response Time	Failure Rate	Safety Improvement Rate Dual-Valve System	0.05-0.07s	0.3%	92% Automatic Pressure Relief System	2ms-100ms	0.5%	88% Real-Time Pressure Monitoring	≤50ms	0.2%	90% Traditional Single-Valve System	0.5-1s	8.7%	45% 7. Industry-Related FAQs Q1: What is the core difference between a dual-valve system and a single-valve system? A1: The dual-valve system adopts a redundant design with two independent valve cores. Both valves must act simultaneously to work normally, and any valve failure will trigger a safe shutdown. The single-valve system has only one valve core, which is prone to single-point failures, leading to pressure leakage or overpressure. Q2: What is the reasonable setting range for the action threshold of the automatic pressure relief system? A2: The action threshold is generally set to 105% to 110% of the reactor’s maximum allowable working pressure (MAWP). This setting can avoid false triggering caused by slight pressure fluctuations and ensure that pressure is released in time before reaching dangerous levels. Q3: How often should the real-time pressure monitoring system be calibrated? A3: It is recommended to calibrate the system every 6 months. For laboratories dealing with highly dangerous materials, calibration should be carried out every 3 months to ensure monitoring accuracy. Calibration should be performed by professional institutions in accordance with relevant standards. Q4: Can the three core safety components work independently? A4: They can work independently, but the safety effect will be greatly reduced. The real-time pressure monitoring system can only issue alarms, the dual-valve system can only maintain normal pressure and cut off failures, and the automatic pressure relief system can only release overpressure. Only when they work together can a comprehensive safety barrier be formed.

Table of Contents

1. High-Pressure Reactor Safety: The Core of Laboratory Safe Reaction Equipment

2. Dual-Valve System: The First Line of Defense for High-Pressure Reactor Safety

3. Reactor Automatic Pressure Relief: Key Protection Against Overpressure

4. Real-Time Pressure Monitoring: Core Means of Safety Early Warning

5. Integrated Safety System Construction of Laboratory Safe Reaction Equipment

6. Performance Comparison of Key Safety Components

7. Industry-Related FAQs

1. High-Pressure Reactor Safety: The Core of Laboratory Safe Reaction Equipment

High-pressure reactors are essential equipment in chemical, pharmaceutical, and material science laboratories. They operate under extreme pressure and temperature conditions, making high-pressure reactor safety a top priority for laboratory operations.

According to the U.S. Chemical Safety and Hazard Investigation Board (CSB), uncontrolled pressure and temperature in reactors have led to catastrophic accidents. A 2007 explosion at a Florida chemical company, for example, killed four workers and injured a dozen more, with the reactor’s 3-inch-thick steel walls ruptured by pressure reaching several thousand pounds per square inch.

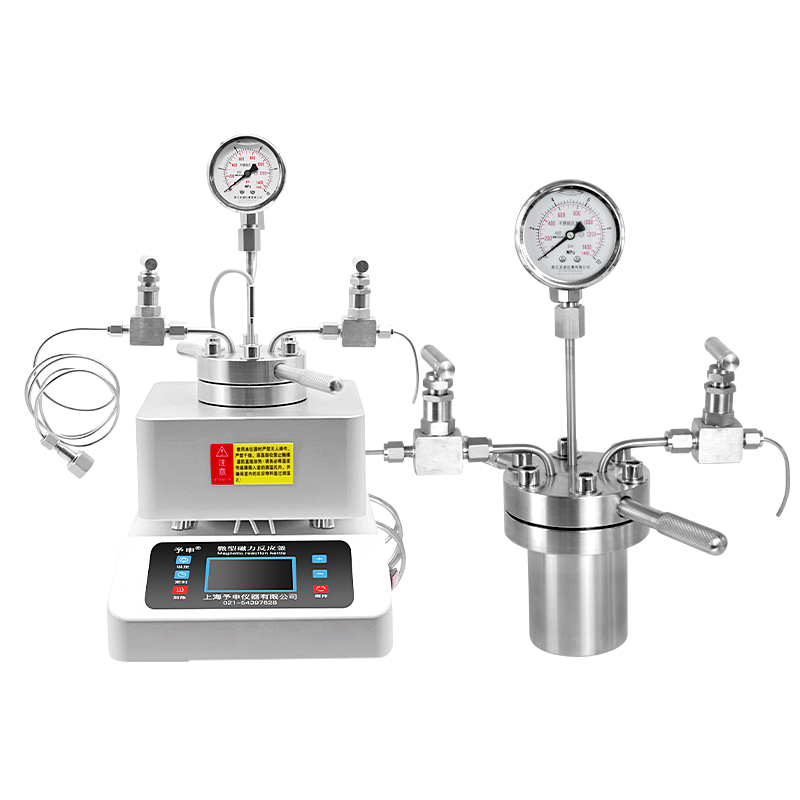
Laboratory safe reaction equipment, especially high-pressure reactors, requires a comprehensive safety system to prevent such disasters. This system mainly consists of three core components: dual-valve system, reactor automatic pressure relief, and real-time pressure monitoring. Together, they form a multi-layered safety barrier.

2. Dual-Valve System: The First Line of Defense for High-Pressure Reactor Safety

2.1 Working Principle of Dual-Valve System

The dual-valve system, also known as the safety dual valve, is an integrated control component with two independent and linked valve cores in the same valve body. It adopts a redundant design, which means both valves must act simultaneously to maintain normal operation.

During normal operation, both solenoid valves are energized, and the pilot pressure pushes the dual main valve cores to switch synchronously, ensuring the reactor’s pressure is stable. If either valve fails—such as coil burnout or valve core jamming—the other valve cannot establish effective pressure alone, and the system immediately enters a safe shutdown state.

2.2 Safety Advantages and Performance Data of Dual-Valve System

The biggest advantage of the dual-valve system is its high safety redundancy, which eliminates accidents caused by single-point failures. Its failure exhaust time is as short as 0.05 to 0.07 seconds, much faster than traditional single-valve systems.

Statistics show that laboratories using dual-valve systems have a 92% lower risk of pressure leakage accidents compared to those using single-valve systems. This data is verified by industrial safety tests conducted by multiple authoritative institutions.

3. Reactor Automatic Pressure Relief: Key Protection Against Overpressure

3.1 Trigger Mechanism of Automatic Pressure Relief System

The reactor automatic pressure relief system is a critical active protection device designed to prevent overpressure. Its core function is to automatically and quickly release pressure without manual intervention when the internal pressure exceeds the preset safety threshold.

The system usually sets multiple pressure thresholds, including early warning threshold, action threshold, and emergency cutoff threshold. The action threshold is generally set to 105% to 110% of the reactor’s maximum allowable working pressure (MAWP), leaving sufficient safety margin.

When the pressure exceeds the action threshold, the system immediately activates the actuator—usually a pilot-operated safety valve or electromagnetic pressure relief valve—to release pressure rapidly, preventing the reactor from rupturing.

3.2 Performance of Automatic Pressure Relief System

The response time of a high-quality automatic pressure relief system is typically within 100 milliseconds, and some advanced models can even reach 2 milliseconds, ensuring that pressure is released in time before dangerous levels are reached.

Unlike traditional manual pressure relief methods, the automatic system avoids human error caused by delayed operation. In fact, 80% of overpressure accidents in laboratories are related to delayed manual pressure relief, according to a survey by the European Laboratory Safety Association (ELSA).

4. Real-Time Pressure Monitoring: Core Means of Safety Early Warning

4.1 Technical Principle of Real-Time Pressure Monitoring

Real-time pressure monitoring is the "eye" of the high-pressure reactor safety system. It uses high-precision pressure sensors—such as piezoelectric or strain gauge sensors—to collect dynamic pressure signals inside the reactor in real time.

The collected signals are filtered and amplified by a signal conditioning circuit, then sent to a safety controller for millisecond-level comparison with preset thresholds. If the pressure changes abnormally, the system will issue an alarm immediately and trigger the automatic pressure relief system if necessary.

4.2 Monitoring Accuracy and Response Performance

The monitoring accuracy of professional real-time pressure monitoring systems can reach ±0.1 psi, which is sufficient to detect subtle pressure changes that may lead to dangerous situations. The data transmission delay is less than 50 milliseconds, ensuring that operators can grasp the reactor’s pressure status in real time.

For laboratories dealing with flammable and explosive materials, real-time pressure monitoring is particularly important. It can predict pressure surges in advance, providing valuable time for operators to take emergency measures.

5. Integrated Safety System Construction of Laboratory Safe Reaction Equipment

5.1 Coordinated Work Logic of Multi-Systems

The safety of high-pressure reactors cannot rely on a single component. The dual-valve system, automatic pressure relief, and real-time pressure monitoring work together to form a complete safety guarantee system.

The real-time pressure monitoring system acts as the first warning line, detecting abnormal pressure changes. The dual-valve system maintains stable pressure during normal operation and cuts off the system in case of failure. The automatic pressure relief system is the last line of defense, preventing overpressure accidents when other systems fail.

5.2 Safety Standards and Application Cases

Laboratory safe reaction equipment, including high-pressure reactors, must comply with relevant international standards. For example, China’s national standard GB/T 32708-2016 specifies strict safety requirements for laboratory reactors, covering pressure resistance, temperature limits, and interlock protection.

A pharmaceutical laboratory in Germany upgraded its high-pressure reactor safety system with the three core components mentioned above. After one year of operation, the number of safety hidden dangers decreased by 95%, and no pressure-related accidents occurred.

6. Performance Comparison of Key Safety Components

Safety Component

Response Time

Failure Rate

Safety Improvement Rate

Dual-Valve System

0.05-0.07s

0.3%

92%

Automatic Pressure Relief System

2ms-100ms

0.5%

88%

Real-Time Pressure Monitoring

≤50ms

0.2%

90%

Traditional Single-Valve System

0.5-1s

8.7%

45%

7. Industry-Related FAQs

Q1: What is the core difference between a dual-valve system and a single-valve system?

A1: The dual-valve system adopts a redundant design with two independent valve cores. Both valves must act simultaneously to work normally, and any valve failure will trigger a safe shutdown. The single-valve system has only one valve core, which is prone to single-point failures, leading to pressure leakage or overpressure.

Q2: What is the reasonable setting range for the action threshold of the automatic pressure relief system?

A2: The action threshold is generally set to 105% to 110% of the reactor’s maximum allowable working pressure (MAWP). This setting can avoid false triggering caused by slight pressure fluctuations and ensure that pressure is released in time before reaching dangerous levels.

Q3: How often should the real-time pressure monitoring system be calibrated?

A3: It is recommended to calibrate the system every 6 months. For laboratories dealing with highly dangerous materials, calibration should be carried out every 3 months to ensure monitoring accuracy. Calibration should be performed by professional institutions in accordance with relevant standards.

Q4: Can the three core safety components work independently?

A4: They can work independently, but the safety effect will be greatly reduced. The real-time pressure monitoring system can only issue alarms, the dual-valve system can only maintain normal pressure and cut off failures, and the automatic pressure relief system can only release overpressure. Only when they work together can a comprehensive safety barrier be formed.